


Most laser buying decisions come down to one question asked the wrong way round. Buyers ask “how thick can this machine cut?” when the question that determines whether the investment pays back is “how thick can this machine cut repeatably, at a cost per metre I can quote against?”
Those are two different numbers, and on mild steel they can differ by 40% or more. A 20 kW fiber laser can sever 60 mm plate. It will not sever 60 mm plate all day, on every sheet, with a dross-free edge a welder can use without grinding.
Its dependable production ceiling on mild steel is closer to 40 mm — and the thickness where it actually earns its keep on cost per part is closer to 10–30 mm.
This guide separates those numbers. It covers what fiber laser cutting does to mild steel and why oxygen changes the physics, the five variables that set the thickness ceiling, a power-tier table built on production thickness rather than marketing maximums, assist gas selection, how mild steel compares to stainless and aluminium, real cutting costs, and where ACCURL’s machines sit against each band.
Key takeaways
- Fiber lasers cut mild steel from roughly 0.5 mm to 50 mm in dependable production; higher figures exist but describe one-off severance, not repeatable output.
- Thickness scales as a power law with an exponent well below 1 — doubling laser power buys roughly a third to a half more thickness, not double.
- 6 kW remains the general-fabrication sweet spot: 25 mm production ceiling, best cost per part in the 3–15 mm band that most job shops live in.
- Oxygen’s exothermic reaction is why mild steel cuts thicker than stainless or aluminium at the same power.
- Oxygen assist pressure falls as thickness rises. Nitrogen pressure rises. Getting this backwards is one of the most common parameter errors on thick plate.
What Is Mild Steel Laser Cutting?
Mild steel laser cutting is a thermal process that uses a focused fiber laser beam and, usually, oxygen assist gas to melt and expel carbon steel along a programmed path — turning Q235, A36 and S235-grade sheet or plate into weld-ready parts.
Oxygen is the standard assist gas because it is fast and economical. It favours cut speed and part cost over a mirror-polished edge, which suits the applications mild steel is chosen for in the first place.
Grades vary by region, so confirm which standard applies to your material before setting parameters: Q235 and SPCC in Chinese-supplied material, A36 in the United States, and S235, S275 and S355 in European structural steel. The process yields a part ready for welding, bending or assembly without secondary edge preparation.
How Does Mild Steel Laser Cutting Work?
One continuous thermal cycle describes it: the focused beam heats a spot past melting point, and assist gas reacts with and ejects the molten material as the beam travels the cut path.
Oxygen reacts exothermically with hot steel.
That reaction adds thermal energy on top of the beam, which is what pushes achievable speed and thickness beyond what the beam alone could deliver.
It also explains the visual signature — oxygen-cut edges are dark and oxidised, nitrogen-cut edges stay bright, because nitrogen is inert and contributes no chemistry, only mechanical ejection.
Before steady-state cutting starts, the machine must pierce the plate. Piercing needs different parameters than cutting, and a pierce optimised purely for speed will compromise the cut that follows it.
Pierce time is negligible on thin sheet but becomes a real cycle-time component from around 10 mm upward, where the beam needs seconds to punch through before the head can begin moving.
On nested thick-plate work with many internal features, total pierce time can exceed total cutting time — which is why pierce strategy, not raw cutting speed, often decides throughput on plate.
What Factors Determine Maximum Cutting Thickness in Mild Steel?
Five variables set the ceiling: laser power, beam quality, material properties, assist gas, and focus position.
- Laser power output. The power-to-thickness relationship is a power law, T = k·P<sup>n</sup>, with n well below 1. Fitted against production-quality thickness on mild steel, n lands in the region of 0.4–0.5; fitted against severance limits it runs higher, nearer 0.65.
Either way the practical consequence is the same: doubling power does not double thickness. Going from 6 kW to 12 kW adds around 20%. Going from 10 kW to 20 kW adds around 60%.
The gain is not even uniform — between roughly 6 kW and 10 kW on mild steel there is a plateau where extra power buys almost no additional thickness, because the limit in that band is melt evacuation from the kerf, not available energy.
Past that plateau, higher power and the larger nozzles and gas flows that come with it start clearing the kerf effectively again, and thickness resumes climbing.
This is why per-kilowatt rules of thumb mislead: there is no constant millimetres-per-kilowatt figure, and any source quoting one has linearised a curve that is not linear.
- Beam quality. A tighter beam concentrates energy into a smaller spot and sustains usable power density through greater depth. Two machines rated at identical wattage can differ materially in thickness capability if their beam parameter products differ.
- Material properties. Mild steel’s low reflectivity at the ~1.06 µm fiber wavelength, combined with its exothermic reaction with oxygen, gives it a higher cutting ceiling than stainless steel or aluminium at equal power.
- Assist gas type and pressure. Oxygen adds thermal energy chemically. Nitrogen and compressed air rely on mechanical ejection alone. Pressure must be matched to thickness and to nozzle bore — see the gas section below, because the direction of that relationship differs by gas and is frequently got wrong.
- Focus position. Focus depth relative to the plate surface sets energy density at the cut front. On a 10 kW machine cutting thick plate, a 2 mm focus error can halve cutting speed. Ultra-high-power systems from 20 kW upward typically require focus shifts in the region of −8 mm to −15 mm on plate over 30 mm. Above roughly 10 kW, thermal lensing becomes a limiting factor in its own right: heat accumulating in the focusing optics drifts the focal point upward by several millimetres during sustained cutting, which is why high-power heads carry temperature sensing and water-cooled optics as standard rather than as options.
Maximum, Stable, or Economic Thickness — Which Number Are You Reading?
Before any thickness table is useful, you need to know which of three numbers it reports. Vendors are rarely explicit, and the gap between them is where most disappointed buyers end up.
- Rated maximum (severance). The thickest plate the machine can pierce and cut through once, under ideal conditions, with an edge nobody promised would be usable. This is the headline number in most marketing material.
- Stable production thickness. What the machine cuts repeatably, shift after shift, with a dross-free weld-ready edge and normal material variation. Typically 70–85% of the rated maximum. This is the number your quoting should be based on.
- Economic cutting thickness. The band where the machine is genuinely cost-competitive — fast enough that cost per metre beats the alternatives. Usually 50–60% of the production ceiling.
Two practical rules follow.
Oxygen-cut mild steel can be run at 80–85% of a machine’s rated maximum and still hold production quality, because oxygen’s thermal contribution gives you margin. Switch to nitrogen or air for a cleaner edge and that safe fraction drops to 65–75%.
Quality also degrades non-linearly. On mild steel there is an edge-quality cliff around 20 mm, above which small parameter errors that were forgiving at 10 mm start producing dross and bevel.
And economically cutting 25 mm mild steel typically needs 12–15 kW — considerably more than a straight-line extrapolation from a 6 kW machine’s capability would suggest.
Two tolerances to plan around: published cutting parameters carry an expected field tolerance of roughly ±10–15%, and batch-to-batch material variation adds another 10–20% swing on top.
How Thick Can Different Fiber Laser Power Levels Cut Mild Steel?
The table below reports production thickness with oxygen assist — repeatable, dross-free, weld-ready — and the economic band where that power tier is genuinely cost-competitive. It does not report severance maximums.
| Laser power | Production thickness (O₂) | Economic band | Notes |
|---|---|---|---|
| 2 kW | 15 mm | 1–8 mm | Thin-to-medium gauge production |
| 3 kW | 20 mm | 1–10 mm | Common job-shop entry point |
| 4 kW | 22 mm | 2–12 mm | Faster thin-gauge throughput than 3 kW; small thickness gain |
| 6 kW | 25 mm | 3–15 mm | The general-fabrication sweet spot |
| 8 kW | 25 mm | 4–16 mm | Speed gain over 6 kW, no thickness gain — evacuation-limited plateau |
| 10 kW | 25 mm | 5–18 mm | Same plateau; buy for speed, not thickness |
| 12 kW | 30 mm | 6–20 mm | Plate work begins here |
| 15 kW | 35 mm | 8–25 mm | Economic 25 mm cutting |
| 20 kW | 40 mm | 10–30 mm | Heavy plate production |
| 30 kW | 50 mm | 12–35 mm | Structural and shipbuilding plate |
Above 30 kW, achievable thickness becomes quality-dependent and application-specific; figures should be established by test cut against your material and edge specification rather than read off a chart.
Nitrogen changes these numbers substantially. On mild steel, nitrogen production ceilings run roughly 60–70% of the oxygen figures above — a 3 kW machine reaching 20 mm on oxygen manages around 12 mm on nitrogen.
You accept that penalty when the part needs an oxide-free edge for painting, coating or cosmetic reasons.
Severance capability sits above all of this.
A 20 kW gantry fiber laser has been demonstrated cutting 60 mm Q235 mild steel with oxygen at approximately 250 mm/min with a 0.8 mm kerf.
That is a real result and it shows what the technology can reach. It is also 50% above the same machine’s 40 mm production figure, at a feed rate no one would quote a production job at. Read it as a capability demonstration, not a specification.
Why Do Cutting Speed and Thickness Trade Off?
Directly, and steeply. Thicker material cuts slower because more dwell time is needed to melt and evacuate material through greater depth.
Push speed at a given thickness and you pay for it in gas consumption, dross, or edge roughness — usually all three.
Reference points across the range:
- a 1 kW laser cutting 1 mm mild steel with oxygen through a 1 mm nozzle at zero focus runs around 3.8 m/min.
- a 2 kW laser on 10 mm Q235 with oxygen runs roughly 1 m/min and produces a grey, weld-ready edge. A 20 kW machine severing 60 mm runs at 0.25 m/min.
The curve is not gentle.
Edge geometry moves with thickness too.
Heat-affected zone on 25 mm mild steel measures around 0.4 mm with oxygen; nitrogen roughly halves that but slows the cut by about 30%.
Thick-plate cuts show bevel up to 4 degrees. Kerf width grows with both thickness and power, from around 0.8 mm on 60 mm mild steel upward.
Two material variants need parameter adjustment. High-carbon steel above roughly 0.3% carbon needs a 15–20% speed reduction and cuts better with nitrogen than oxygen.
Galvanized steel needs a 15–25% speed reduction plus deliberate fume-extraction attention, because the zinc coating vaporises in the cut.
Which Assist Gas Should You Use for Mild Steel?
Three gases, three trade-offs between speed, edge quality and cost.
Oxygen is the default because its exothermic contribution delivers speed and thickness the other two cannot match.
- Oxygen — choose for speed and thickness. Minimum 99.5% purity. Produces a dark, oxidised, weld-ready edge and consumes the lowest gas volume of the three, around 20 m³/h on 10 mm steel. A 3 kW laser on 6 mm mild steel runs roughly 3.5 m/min with oxygen against 2.2 m/min with nitrogen.
- Nitrogen — choose for an oxide-free edge that takes paint or coating without preparation. Minimum 99.99% purity. Consumes roughly five times the volume of oxygen at equal thickness, around 100 m³/h on 10 mm steel. On any significant nitrogen volume, a pressure swing adsorption generator typically pays back against bottled supply in 9–26 months.
- Compressed air — roughly 78–80% nitrogen and 20–21% oxygen. Cuts gas cost by 80–90% against nitrogen but stays limited to thinner sections and cannot produce an oxide-free or mirror finish.
Getting Assist Pressure the Right Way Round
The two gases move in opposite directions as thickness increases, and this is a common source of parameter error.
- Oxygen pressure falls as thickness rises. Thin gauge runs relatively high pressure through a small nozzle. Thick plate runs low pressure — often below 1.5 bar on 20 mm and above — through a large-bore nozzle. The reason is chemical: on thick plate the exothermic reaction is already supplying substantial energy, and excess oxygen flow drives self-burning, widening the kerf and destroying edge quality rather than improving evacuation.
- Nitrogen pressure rises as thickness rises, from single-digit bar on thin sheet to 20 bar or more on thick section, because nitrogen has no chemistry to contribute and must clear the kerf by mechanical force alone.
Pressure must always be matched to nozzle bore and standoff, not raised in isolation.
Increasing pressure without opening the nozzle causes boundary layer separation in the gas jet — the flow detaches from the kerf wall, molten material gets trapped against it, and you get dross that looks like insufficient pressure and tempts you to raise it further.
If dross appears after a pressure increase, the nozzle is the variable to change, not the regulator.
Verify all pressures against your machine’s cutting database before production. The figures above describe general fiber laser practice; head design, nozzle geometry and control system differ enough between machines that manufacturer parameter tables take precedence.
How Does Mild Steel Compare to Stainless Steel, Aluminium and Copper?
Gas chemistry is the whole story. Oxygen’s exothermic boost lets mild steel cut noticeably thicker than any of the following at equal power, all of which are cut with nitrogen.
| Metal | Thickness relative to mild steel at equal power | Key difference |
|---|---|---|
| Stainless steel (304, 316, duplex) | Around 60–70% | Nitrogen-assisted, no exothermic boost. Duplex needs 20–30% lower speed. Batch variation adds 10–20%. |
| Aluminium | Around 60–70%, with poor returns on extra power | High reflectivity at ~1.06 µm and high thermal conductivity; needs roughly 30–40% more power for equivalent results |
| Copper and brass | Typically under 20 mm even at high power | Extreme reflectivity; often needs 12–20 kW, or a green-wavelength module with beam dump and reduced power during pierce |
Cutting stainless with compressed air instead of nitrogen needs roughly 20–30% more power and still will not reach nitrogen’s finish.
How Much Does Mild Steel Laser Cutting Cost?
Cutting 10 mm mild steel on a 6 kW fiber laser with oxygen assist costs approximately $0.49 per metre of cut, built from a total machine rate of about $73 per hour — roughly $13/hr in operating cost, $25/hr in machine amortisation and $35/hr in loaded operator labour.
The same cut on nitrogen runs about $1.02 per metre, and thin-gauge work at 3 mm drops to around $0.15 per metre.
However, cost per part is not a portable figure — it depends entirely on cut length, pierce count and nest efficiency, so a per-part number from one job tells you nothing about another.
The two units that transfer between jobs and between machines are cost per metre of cut and cost per machine-hour.
The figures above assume US industrial electricity at $0.13/kWh, bulk liquid oxygen at $0.25/m³, bulk liquid nitrogen at $0.30/m³, a loaded operator rate of $35/hr, and amortisation of a $250,000 installed 6 kW system over 10,000 productive hours.
Substitute your own rates — the structure holds even where the numbers don’t.
| Component | 6 kW @ 10 mm, oxygen | Notes |
|---|---|---|
| Electricity | $2.90/hr | ~22 kW total system draw including chiller, extraction and drives |
| Assist gas | $5.00/hr | ~20 m³/h oxygen |
| Consumables | $3.00/hr | Nozzles, protective windows, lens amortisation |
| Routine maintenance | $2.00/hr | |
| Operating subtotal | $12.90/hr | |
| Machine amortisation | $25.00/hr | $250k over 10,000 hours |
| Operator labour | $35.00/hr | Loaded rate |
| Total machine rate | $72.90/hr |
At 2.5 m/min on 10 mm with oxygen — 150 metres of cut per hour — that machine rate divides down to $0.49 per metre. Note that labour and amortisation together account for 82% of it.
Operating cost is the smaller half of the picture on medium gauge, which is why utilisation and automation move the number more than gas selection does at this thickness.
How cost per metre moves with thickness
| Job | Machine rate | Cutting speed | Cost per metre |
|---|---|---|---|
| 3 mm, 6 kW, oxygen | ~$73/hr | ~8 m/min | ~$0.15 |
| 10 mm, 6 kW, oxygen | ~$73/hr | ~2.5 m/min | ~$0.49 |
| 10 mm, 6 kW, nitrogen | ~$98/hr | ~1.6 m/min | ~$1.02 |
| 25 mm, 15 kW, oxygen | ~$100/hr | ~0.6 m/min | ~$2.78 |
Cost per metre rises far faster than thickness because speed collapses while the hourly rate barely moves. Going from 3 mm to 25 mm is an 8× thickness increase and an 18× cost-per-metre increase.
Gas is where the choices are, and the effect is largest on thin and medium gauge where it represents a meaningful share of a low per-metre cost.
- Oxygen at ~20 m³/h on 10 mm costs about $5/hr on bulk supply. Cheapest of the three per hour, and the fastest.
- Nitrogen at ~100 m³/h costs about $30/hr on bulk liquid — six times oxygen — and cuts roughly 35% slower on mild steel. That combination is what doubles cost per metre.
- On-site PSA nitrogen generation brings nitrogen down to roughly $0.05/m³, or about $5/hr. That saves around $25/hr against bulk liquid; at 2,000 nitrogen-cutting hours a year, a $60,000–120,000 generator pays back in roughly 12–24 months.
- Compressed air costs around $2.50/hr at equivalent flow — an 80–90% saving against bulk nitrogen — but is limited to thinner sections and cannot produce an oxide-free or mirror finish.
Bottled nitrogen is a different economic category entirely. At typical cylinder pricing, 100 m³/h is not a production proposition; it is why every shop running volume nitrogen work moves to bulk or generation.
Machine investment by power tier
Installed system prices vary widely by region, configuration and automation, but the relative scaling is consistent:
| Power | Typical installed cost |
|---|---|
| 3 kW | $80,000–150,000 |
| 6 kW | $150,000–250,000 |
| 12 kW | $250,000–400,000 |
| 20 kW | $400,000–700,000 |
| 30 kW, large format | $700,000–1,200,000+ |
At 2,000 hours a year over five years, every $100,000 of machine cost adds $10/hr to the machine rate. Run two shifts and that halves — which is the real argument for automation, since it moves the largest line in the model.
Against plasma
A 100 A plasma system on 10 mm mild steel runs roughly $0.30–0.40 per metre — cheaper than laser’s $0.49, and the gap widens on heavier plate where plasma’s speed advantage grows. Lower machine cost is most of the difference; plasma consumables run higher per hour, but amortisation runs far lower.
Laser wins on kerf width, taper, heat-affected zone and part accuracy at every thickness. The comparison is only meaningful if your part tolerance genuinely permits plasma quality — and if it does, on plate above 25 mm, plasma usually is the right answer.
For reference, job shops typically charge out laser time at $100–250/hr depending on power tier and region, against the ~$73/hr internal rate modelled above.
Does Higher Laser Power Pay Off?
Weigh the investment premium of the next tier against how often you would genuinely use the thickness it buys, and size power to the range you cut most days rather than to your worst-case job.
For occasional thick-plate work, outsourcing or plasma is almost always cheaper than carrying idle capacity year-round. Waterjet suits occasional thick or heat-sensitive jobs, being a cold process with no heat-affected zone.
The counter-argument is speed, not thickness. Moving from 6 kW to 10 kW buys no additional mild steel thickness, but it substantially raises cutting speed across the thin-to-medium band. If your volume is in 3–10 mm, that speed gain — not a thickness number — is what justifies the tier.
How to Run a Test Cut Before Committing an Unfamiliar Thickness
Before putting a new thickness into production, run this in under an hour.
- Use production material. Same grade, same supplier, same batch condition including mill scale. Scale-free test coupons will flatter the result.
- Establish the pierce first. Confirm a repeatable pierce with an acceptable crater before touching cutting parameters. If the pierce is marginal, nothing downstream is valid.
- Bracket the speed. Cut three 300 mm straight lines at the parameter-table speed, 15% below, and 15% above. This maps where your quality boundary sits inside expected field tolerance.
- Test geometry, not just straight lines. Include a small hole at roughly 1× thickness diameter, an internal corner, and a narrow tab. These fail before straight cuts do and reveal whether the thickness is genuinely production-viable.
- Inspect the underside. Dross adhesion on the bottom edge is the primary pass/fail. Check bevel angle and kerf width against part tolerance while you are there.
- Repeat once, cold and once warm. Run the same test after 30 minutes of continuous cutting. Thermal lensing shows up here and nowhere else.
- Record the result against the nest, not just the parameters. Pierce count and cut length determine whether the thickness is economically viable, not only technically achievable.
Does ACCURL Laser Cutters Fit for Mild Steel Applications?
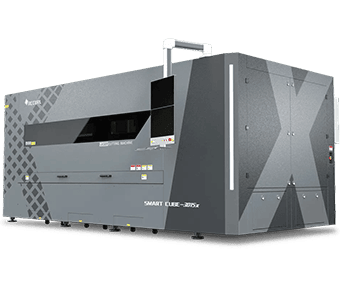
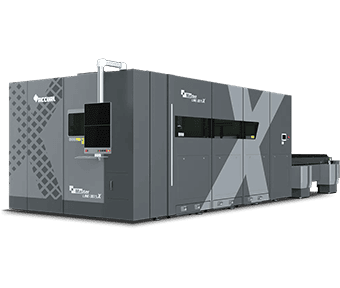
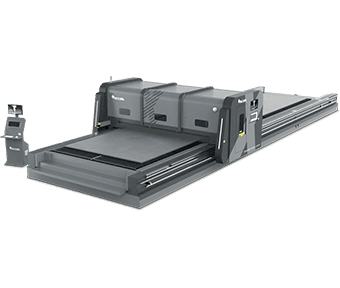
Three ACCURL laser cutter series cover the mild steel range, and each maps to one of the power bands above.
SmartLINE — 2 kW to 4 kW
Thin-to-medium gauge production, up to a 20 mm production ceiling on oxygen. This is the job-shop machine: the economic band of 1–12 mm covers the majority of general fabrication work, and the machine is configured for throughput in that range rather than for plate.
Precitec LightCutter head with automatic focus, Rexroth linear guides, ALPHA hardened helical rack and pinion, Yaskawa EtherCAT servos. Automatic pallet exchange completes a table change in 15 seconds or less.
Both nitrogen and oxygen supply lines with proportional valve control, so switching between weld-ready oxygen cutting and oxide-free nitrogen cutting is a program setting rather than a changeover. HypCut FSCUT8000 control.
MasterLINE — 6 kW to 15 kW
The sweet-spot platform, spanning the 25 mm production ceiling at 6 kW through to 35 mm at 15 kW. This covers both the highest-value general fabrication band and the entry to genuine plate work.
Beckhoff EtherCAT servos, Precitec ProCutter Zoom 2.0 head with motorised focus adjustment, zoom optics for automatic focus diameter control, permanent protective window monitoring and automated piercing.
The zoom optics matter specifically for mild steel: they allow beam size and angle of incidence to be matched to thickness, which widens the kerf enough to clear melt on the thicker end of the range — directly addressing the evacuation limit described earlier.
Automatic nozzle self-cleaning after a set contour count. Double pallet changer, eight-zone ducted extraction, cast aluminium gantry, Libellula.CUT nesting. Loader and unloader automation available for lights-out operation.
SMART ECO (SE Series) — 6 kW to 60 kW
This is the structural steel, shipbuilding and heavy equipment machine.
Working areas span from 9,000 × 3,000 mm to 21,000 × 3,000 mm, extendable in 3,000 or 6,000 mm segments to a maximum of 26,000 mm.
Published mild steel thickness by laser source: 6 kW / 25 mm, 8 kW / 25 mm, 10 kW / 25 mm, 12 kW / 30 mm, 15 kW / 35 mm, 20 kW / 40 mm, 30 kW / 50 mm. Above 30 kW, maximum thickness is quality-dependent and quoted on request. Note that the 6–10 kW plateau in this chart is the evacuation-limited region described earlier, not a data error — it is what the physics actually does.
Three features bear directly on mild steel economics:
- ACCURL LasGAM gas control (with HOERBIGER) adjusts O₂ content from 0 to 20% in under a second, targeting the largest variable cost in the model above. Rated at up to 50% more output and up to 55% less cutting gas consumption against standard processes, with continuous status monitoring.
- Automatic nozzle changing removes manual change and recalibration, allowing different material thicknesses in a single unattended pass — which matters on mixed-thickness plate nests where nozzle bore must track thickness.
- Steel crossbeam with intelligent lubrication, chosen over aluminium for large spans: 35% weight reduction with 0.04 mm deflection at 1.0 G acceleration.
Conclusion
Mild steel is the most forgiving material a fiber laser cuts, and oxygen is why. The exothermic reaction adds thermal energy no other common material gets, pushing the production ceiling from roughly 15 mm at 2 kW to 50 mm at 30 kW — consistently thicker than stainless or aluminium at the same power.
But the number that should drive your decision is not the ceiling. It is the economic band beneath it, where cost per metre is low enough to win work. A 6 kW machine reaches 25 mm and earns its money between 3 and 15 mm. A 20 kW machine reaches 40 mm and earns its money between 10 and 30 mm.
So size power to the thickness you cut most days, not the thickest sheet you have ever quoted. Then confirm it with a test cut on production material before the first job depends on it.